Technical Consultation & On-Site Support
Work directly with experienced filtration professionals to evaluate your application, troubleshoot performance issues, and identify the right solution for your process.
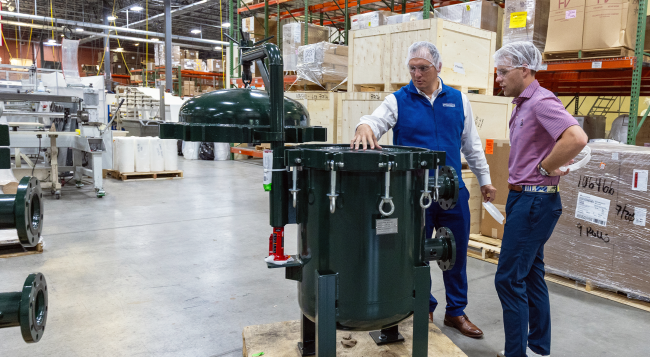
Practical Filtration Guidance
The right filtration solution depends on more than a micron rating. Fluid characteristics, contaminant type, flow rate, temperature, pressure, housing configuration, product-quality requirements, and operating costs all influence filter performance.
Strainrite’s technical and commercial teams work with customers to understand these factors and recommend an appropriate filter media, construction, configuration, and system design.
Technical Consultation
Whether you are selecting a filter for a new application or troubleshooting an existing process, our team can help evaluate the available information and determine the appropriate next step.
Consultation may include:
Filter media and micron-rating selection
Chemical and temperature compatibility
Housing and filter-element sizing
Filter-life and differential-pressure concerns
Product-quality or clarity requirements
Comparative product evaluations
Opportunities to reduce filtration costs
When additional information is needed, we may recommend sample testing, filter analysis, or an on-site assessment.
On-Site Support
Some filtration challenges are best understood at the point of use. When appropriate, Strainrite territory managers, technical personnel, or authorized representatives can visit your facility to review the existing filtration process and operating conditions.
An on-site visit may include an evaluation of the current filters, housings, flow requirements, change-out practices, performance concerns, and process objectives. Our team then works with you to identify practical opportunities for improvement.
Custom Filtration Solutions
When a standard product does not meet the application’s requirements, Strainrite can evaluate custom filter and housing options.
Our capabilities include application-specific filter media, alternative dimensions and configurations, custom end treatments, specialty materials, and filtration housings designed around the customer’s process requirements.
Every custom solution begins with understanding the application and determining whether a modified or purpose-built product can create meaningful operational value.
Direct Access to Our Team
As a family-owned manufacturer based in Auburn, Maine, Strainrite gives customers direct access to the people responsible for recommending, designing, and manufacturing their filtration products.
Our territory managers, customer-service team, technical personnel, and manufacturing specialists work together to respond to questions, evaluate challenges, and support customers throughout the life of the application.
The Strainrite Advantage

Deep Filtration Science
Over four decades of R&D and field experience in liquid filtration technology. Our team brings unmatched expertise to filter selection, media compatibility, and process optimization.

Consultative Approach
We don’t just sell filters — we partner with you. Our holistic needs assessments evaluate your entire filtration process to deliver solutions that reduce costs, improve quality, and increase efficiency.

Nationwide Field Coverage
Territory sales managers across every region of the U.S. — plus international coverage in Canada, Mexico, Europe, and Latin America — ensure expert support is always within reach.

Quality & Compliance Assurance
ISO 9001-certified manufacturing, third-party validated clean rooms, and comprehensive testing (X-ray, ultrasonic, hydrostatic) ensure every product meets the highest industry standards.
Why Strainrite for Scientific Consultation & On-Site Support
47+ Years of Filtration Leadership
Founded in 1978, Strainrite’s heritage is closely tied to the initial development of filter bag technology. Our founder, John H. Lapoint Jr., was instrumental in conceiving, perfecting, and proliferating the original filter bag — and that pioneering spirit drives everything we do today.
Industry-Specific Expertise
From pharmaceuticals and food & beverage to oil & gas and microelectronics, our technical team understands the unique regulatory, process, and quality requirements of your industry. We serve leading coatings and ink producers worldwide and supply filtration to customers in over 40 countries.
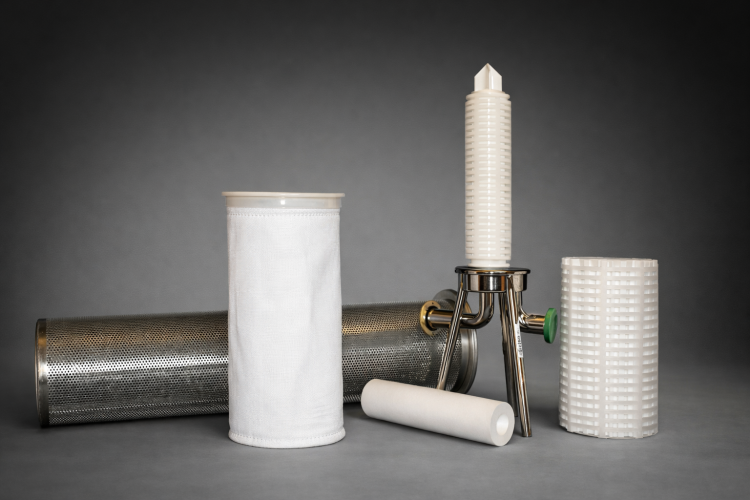
Validated & Certified Solutions
Our products are manufactured and tested in third-party validated clean rooms under an ISO 9001-certified quality management system. We provide validation guides, bacterial retention testing, USP Class VI compliance, and LAL endotoxin documentation to help you satisfy regulatory requirements.
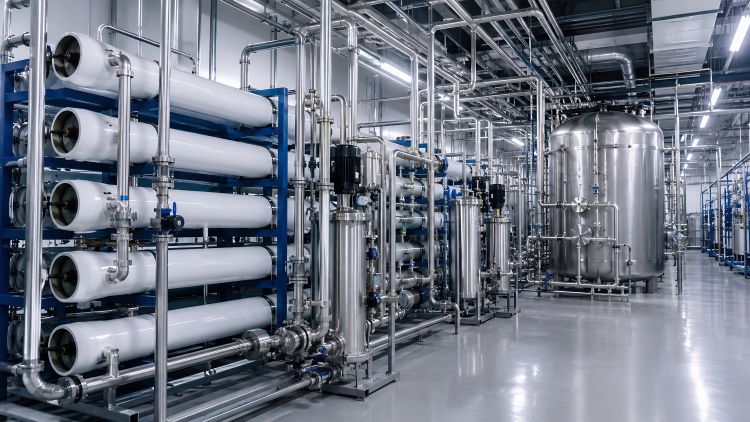
Custom Engineering Capabilities
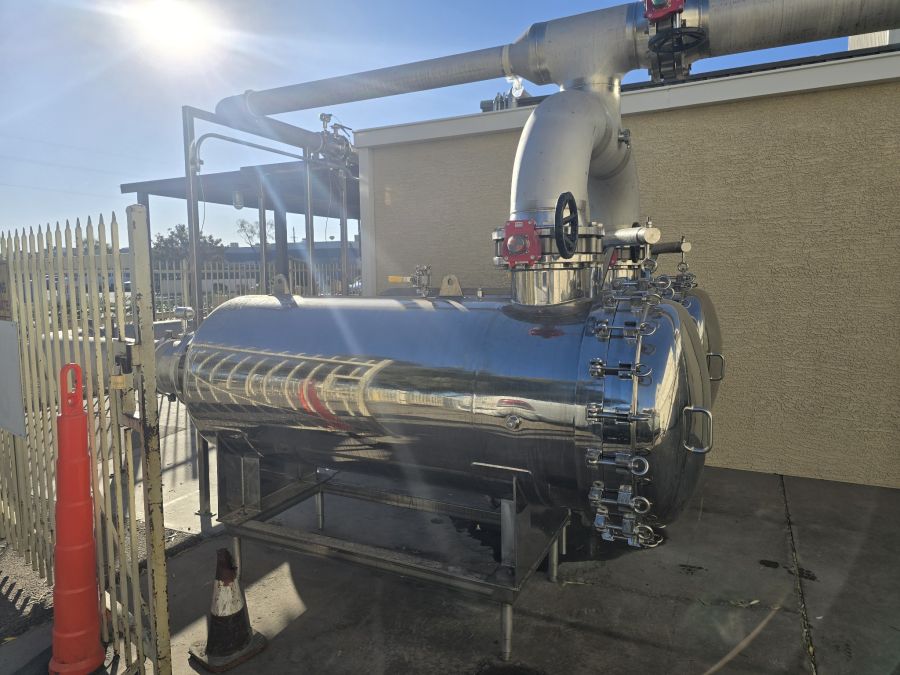
Our engineering team designs custom filtration systems for special requirements, including electropolished finishes, code 7 & code 6 cartridge configurations, stainless steel systems with legs, and sterilization via hot water or in-line steam. If a standard solution doesn’t exist, we build one.
Fast Delivery & Reliable Supply
While competitors may take six months to a year to ship, Strainrite delivers faster. Our domestic manufacturing in Auburn, Maine, combined with deep inventory and efficient production processes, ensures you get the products you need when you need them.
How We Work With You
Understand the Process
We begin by discussing the fluid, contaminant, operating conditions, existing equipment, current performance, and desired result.
Evaluate the Options
Our team reviews the available information and determines whether the application calls for a standard product, additional testing, an on-site assessment, or a custom solution.
Recommend the Next Step
We provide a practical recommendation based on filtration performance, implementation requirements, and total operating cost.
Review The Results
Following a trial or product change, we remain available to review performance and recommend adjustments when necessary.
Speak With a Filtration Specialist
Have a new application or an existing filtration process that is not performing as expected? Contact Strainrite to discuss the challenge with an experienced member of our team.
Related Blog Posts
Explore our latest insights on filtration technology and best practices.
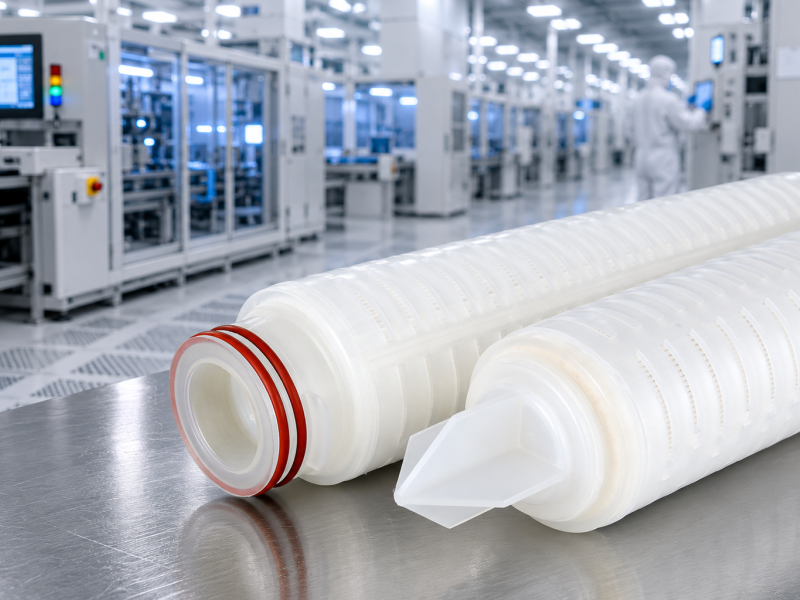
Strainrite Cartridge Components Upgraded to a Higher-Temperature Grade of 220°F (104° Celsius)
Strainrite Upgrades Polypropylene Cartridge Hardware to a Higher-Temperature Grade
Read More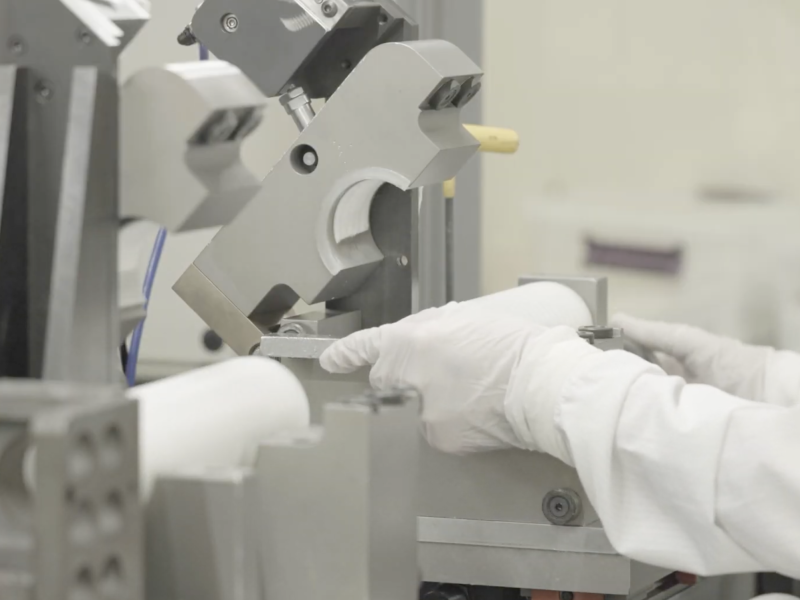
Strainrite Expands Cleanroom by 625 SQ/FT
Strainrite is expanding its cleanroom by 625 square feet by the end of Q3, adding capacity for new manufacturing equipment arriving in 2027
Read More
Gamma Irradiated Clarity Capsules & Cartridges Reach a New 4-Year Shelf-Life Milestone
Gamma Irradiated Clarity Capsule and Cartridge filters have successfully completed 4-year shelf-life validation testing
Read More