About About Us

Nearly 50 Years of Filtration Expertise

Since 1978, The Strainrite Companies has partnered with manufacturers around the world to engineer liquid-filtration solutions that improve product quality, protect critical equipment, increase process yields, and deliver lasting operational value.

Our History

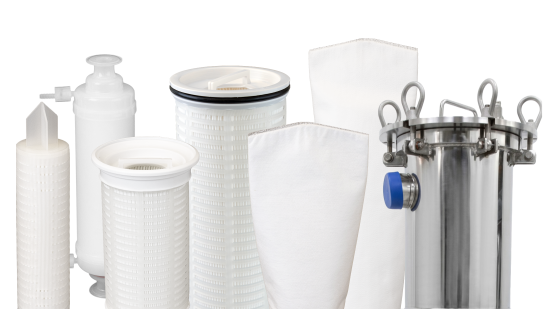
Strainrite is a family-owned liquid-filtration manufacturer based in Auburn, Maine. For nearly five decades, we have designed and manufactured filter bags, cartridges, capsules, and housings for demanding applications across a wide range of industries.

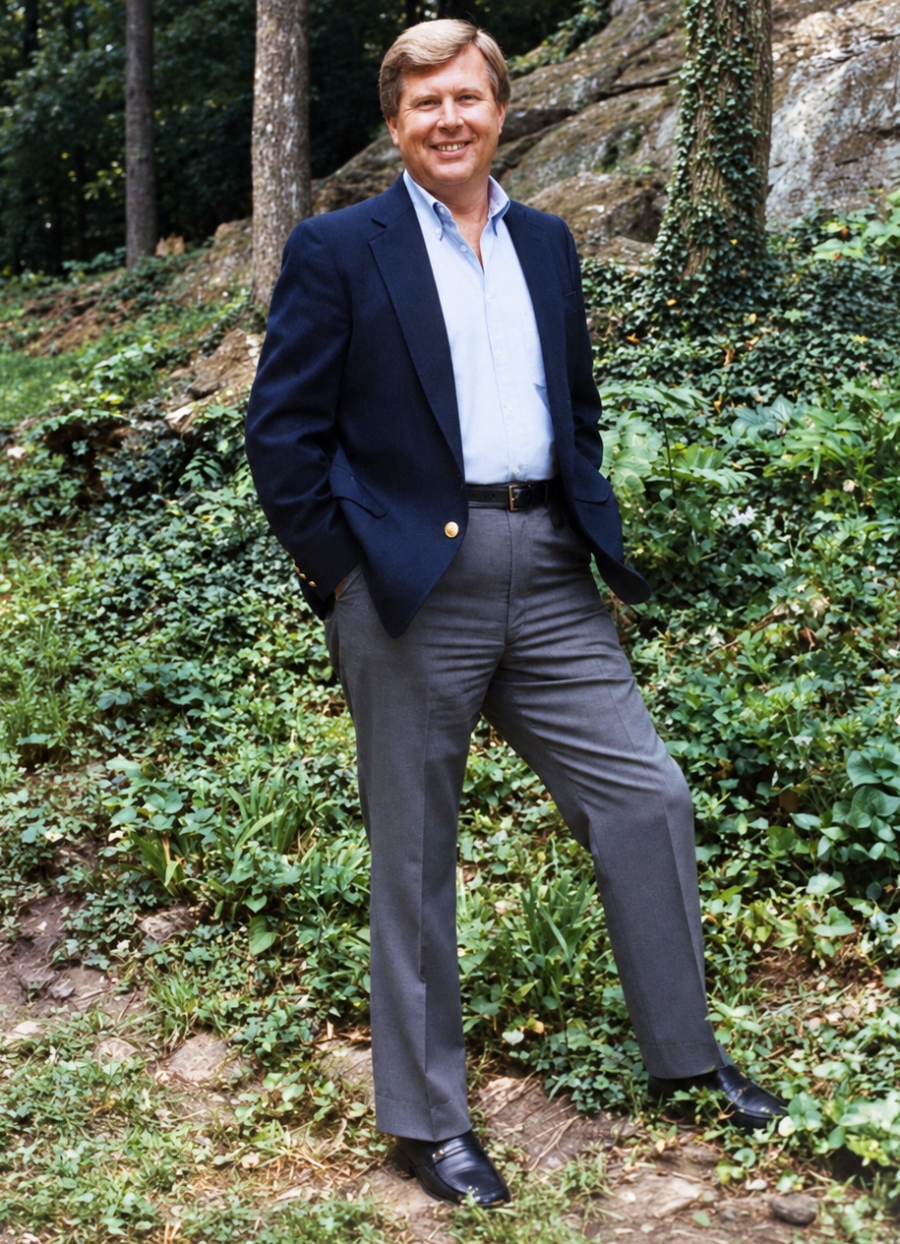
Our history is closely connected to the early development of liquid filter-bag technology. Strainrite founder John H. Lapoint Jr. helped pioneer the design and adoption of the modern liquid filter bag—establishing a foundation of filtration expertise that continues to guide the company today.

Since our incorporation in 1978, Strainrite has grown from those filter-bag roots into a global filtration partner serving customers throughout the United States and in more than 40 countries. Although our capabilities have expanded, our approach remains the same: understand the customer’s process, identify the true source of the filtration challenge, and develop the right solution for the application.

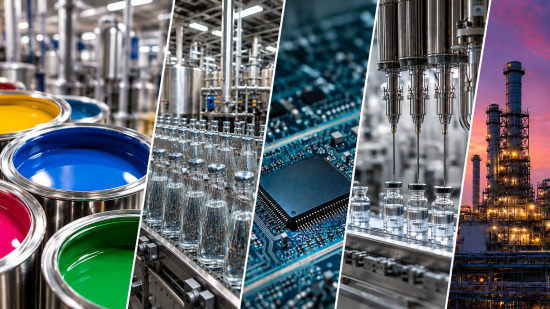
Today, Strainrite products help manufacturers ensure finished-product quality, protect equipment, improve process yields, and reduce operational costs across industries including pharmaceutical and life sciences, food and beverage, paints, coatings and inks, oil and gas, microelectronics, and more.

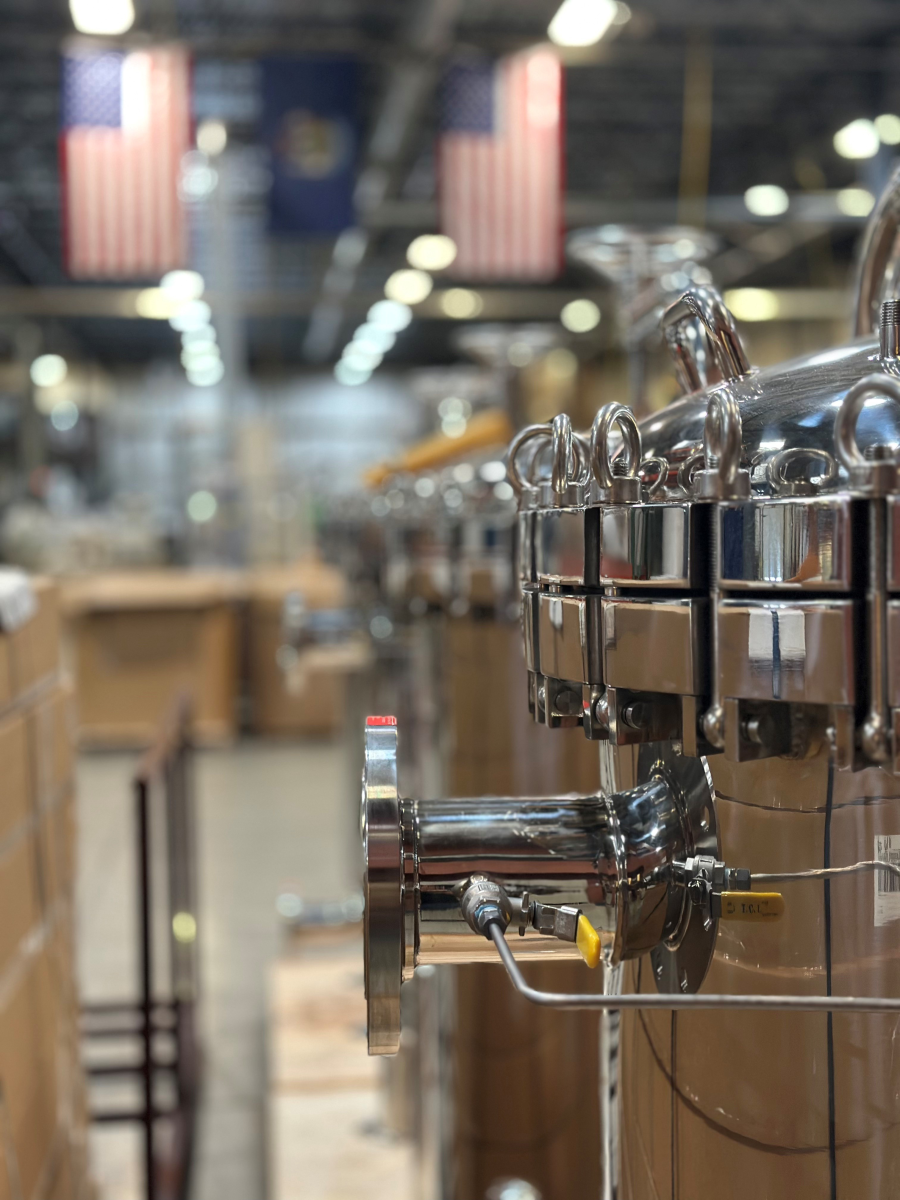
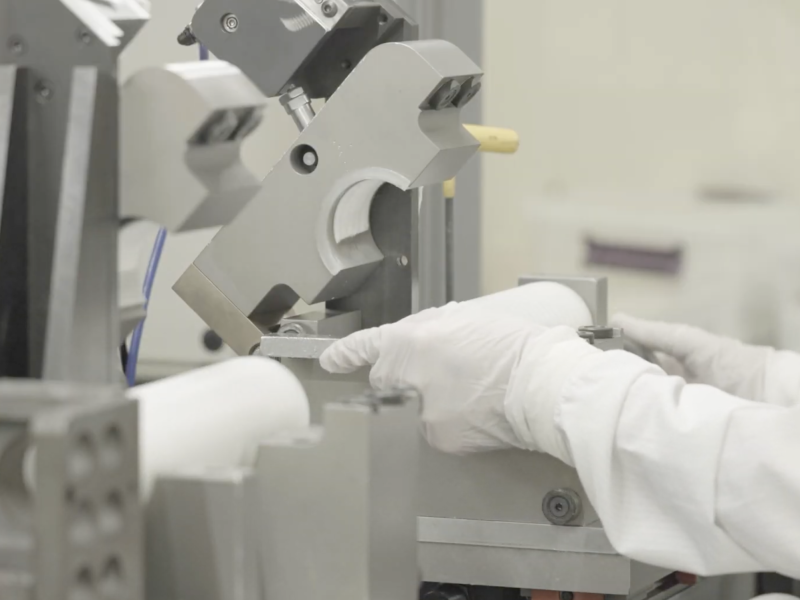
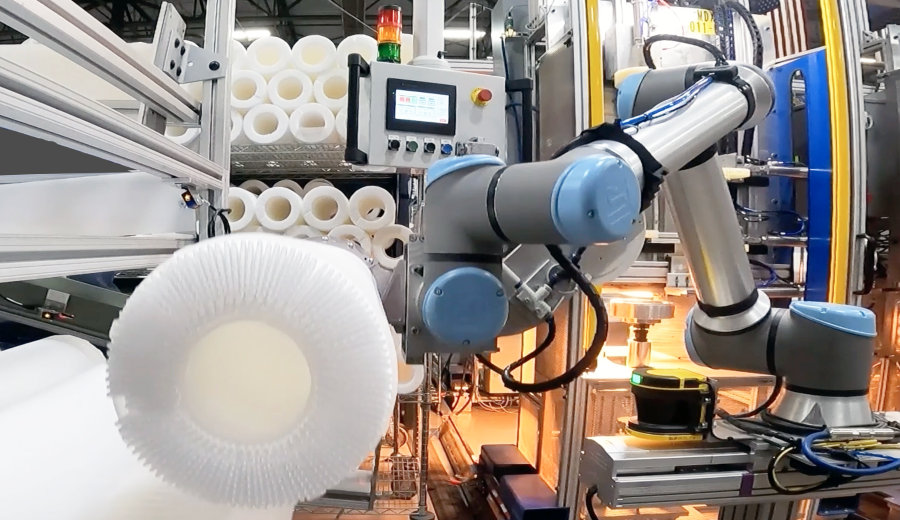
Our products are manufactured at our 81,000-square-foot facility in Auburn, Maine. Our silicone-free, cGMP third party accredited, ISO 9001:2015-certified manufacturing environment supports consistent quality, dependable lead times, and products designed for use in highly controlled applications.
Our Mission

Our mission is to solve liquid-filtration challenges through technical expertise, dependable manufacturing, and close customer collaboration.

We work alongside our customers to understand their processes and engineer solutions that improve finished-product quality, reduce waste, increase throughput, and lower total filtration costs. As a family-owned manufacturer, we measure our success not simply by the products we ship, but by the long-term value those products create for our customers.

Our Values

  • Science First:
    We use engineering, testing, and processing data to develop and validate filtration solutions.

  • Service Beyond the Sale:
    We invest the time required to understand each customer’s process, operating conditions, and objectives—not simply the product currently being used.

  • Partnership Over Transactions:
    Our technical and commercial teams work alongside customers to improve filtration performance, reduce filter consumption, minimize change-out labor, and lower total operating costs.

  • Relentless Quality:
    From material selection through final inspection, we hold every product to demanding quality standards and manufacture within an ISO 9001:2015-certified quality-management system.

  • Innovation With Purpose:
    We develop filtration technologies that solve practical customer problems—improving throughput, extending service life, reducing waste, and creating measurable operational value.

Sustainability Through Better Filtration

At Strainrite, sustainability is closely connected to filtration efficiency. A solution that extends filter life, increases product recovery, reduces change-out frequency, or improves throughput can help customers consume fewer materials, use less energy, and send less waste to landfill.

Our team works with customers to evaluate the entire filtration process—not simply the cost of an individual filter. By properly sizing filtration systems, selecting the right media, and developing application-specific solutions, we help reduce filter consumption, product loss, labor requirements, and process downtime.

We believe the most sustainable filtration solution is one engineered correctly for the application: delivering consistent product quality, reliable performance, and a smaller environmental footprint over its operating life.

Our team will work with you to understand your process and identify a solution that improves performance and lowers total operating costs.

Why Choose Strainrite

Consultative Application Support

Over 47 years of experience serving highly regulated and demanding industries; family-owned and operated since 1978.

U.S. Manufacturing Excellence

All products are manufactured in our 81,000 sq. ft. ISO-certified facility in Maine - ensuring consistent quality, short lead times, and rapid customization from pilot to production.

Comprehensive Filtration Portfolio

A full range of filtration solutions across every stage of the process, including sterile liquid filtration and gas/vent technologies.

Industry Leadership

Over 47 years of experience serving highly regulated and demanding industries; family-owned and operated since 1978.

Engineered Systems & Assemblies

Custom manifolds, specialty vessels, and integrated filtration systems designed to meet unique operational, quality, and regulatory requirements.