
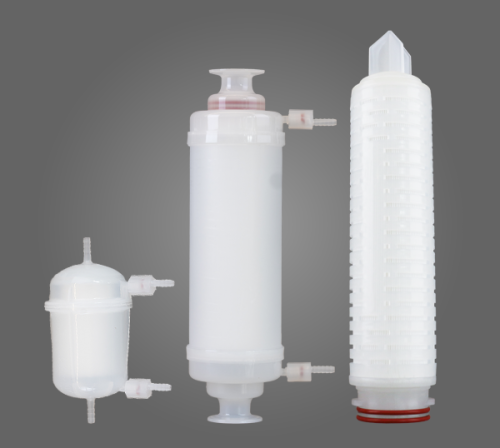
Clarity™ Cartridges & Capsules
Nominal-and absolute-rated cartridges and capsules engineered for clarification, prefiltration, final filtration, and critical-process applications.
Since 1978, Strainrite has engineered and manufactured liquid-filtration solutions that improve product quality, increase process yields, protect critical equipment, and reduce total operating costs.
Nominal-and absolute-rated cartridges and capsules engineered for clarification, prefiltration, final filtration, and critical-process applications.
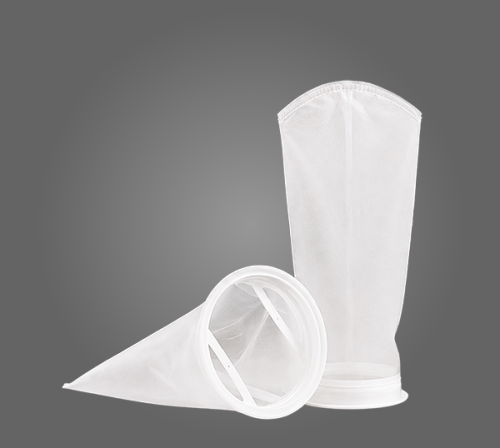
From dependable felt and mesh bags to extended-life and high-efficiency designs, our filter bags deliver reliable performance across demanding liquid applications.
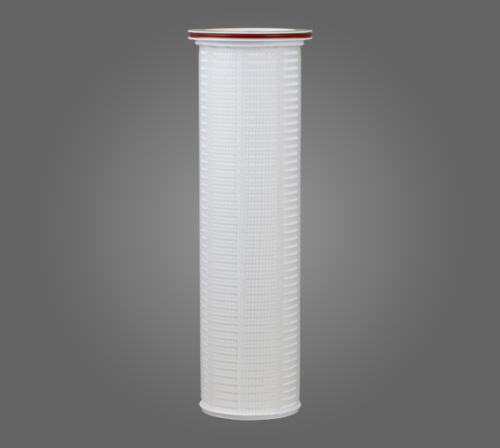
High-capacity filtration elements are engineered to increase throughput, extend service life, and reduce filter-change frequency in demanding applications.
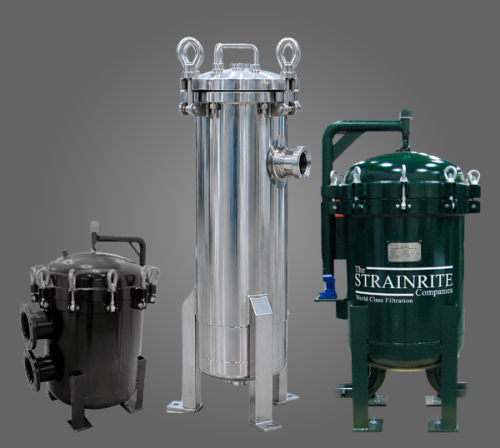
Standard and custom-engineered filtration housings—designed around your flow rate, process conditions, and operating requirements.

Application-specific filtration for buffer and media preparation, prefiltration, bioburden reduction, critical final filtration, and process venting, supported by validation documentation.
Pharmaceutical & Life Sciences
Filtration solutions that protect product quality, improve clarity, and support efficient processing across food, beverage, brewing, distilling, bottling, and ingredient manufacturing.
Food & Beverage
Reliable filtration for chemical and API manufacturing, including raw-material clarification, catalyst recovery, contaminant removal, intermediate processing, and downstream equipment protection.
Chemicals & API
High-capacity filtration that removes agglomerates and unwanted contaminants, improves finished-product quality, protects filling equipment, and extends production runs.
Inks, Paints, and Coatings
Durable filtration that maintains fluid quality, protects critical equipment, and reduces downtime across upstream, midstream, and downstream oil and gas operations.
Oil & Gas
Particulate filtration for cooling towers, chilled-water systems, coolant distribution units, and liquid-cooling loops—protecting heat-transfer equipment and maintaining system performance.
Data Centers

Nearly five decades of application experience inform every recommendation. Our team combines practical process knowledge with a science-based approach to filtration problem-solving.

We don’t force an off-the-shelf product into every process. We evaluate your application, operating conditions, and goals to identify—or engineer—the right filtration solution.

As a family-owned manufacturer in Auburn, Maine, we respond quickly, communicate directly, and remain involved from initial evaluation through implementation and ongoing support.

Our solutions are designed to improve product quality, increase throughput, extend filter life, reduce downtime, and lower total filtration costs.
Service is our focus
The right filtration solution starts with understanding the process. Strainrite works with customers to evaluate fluid characteristics, contaminant loads, flow requirements, operating conditions, product-quality objectives, and total filtration costs.
Whether the answer is a standard product, a system retrofit, or a custom-engineered solution, our goal is the same: deliver measurable improvements in filtration performance and long-term operating value.
Whether you are developing a new process, replacing an existing filter, addressing inconsistent product quality, or looking to reduce filtration costs, our team can help identify the right next step.
See how manufacturers have improved product quality, resolved process challenges, and reduced operational risk with Strainrite.
In October 2024, a leading manufacturer of specialty ingredients, including natural vitamin E, faced significant supply chain delays in obtaining their usual filtration products for vitamin E oil processing — threatening to disrupt their production schedule.
A leading industrial coatings manufacturer developing an innovative isopropyl alcohol-based product required absolute optical clarity in their formulation. During lab-scale development, an unexpected haze — later identified as suspended salts 1–5 microns in size — threatened the launch and prompted a search for a reliable filtration partner.
Stay up to date with the latest from Strainrite
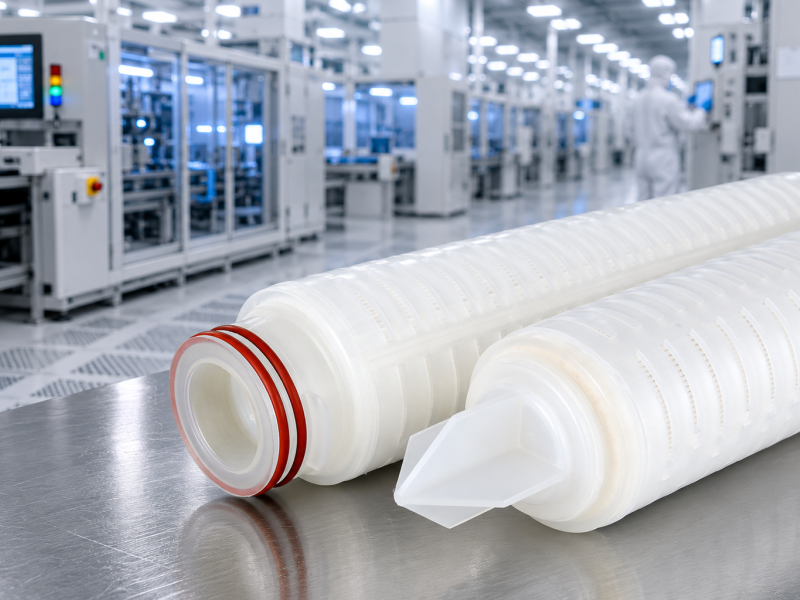
Strainrite Upgrades Polypropylene Cartridge Hardware to a Higher-Temperature Grade
Read More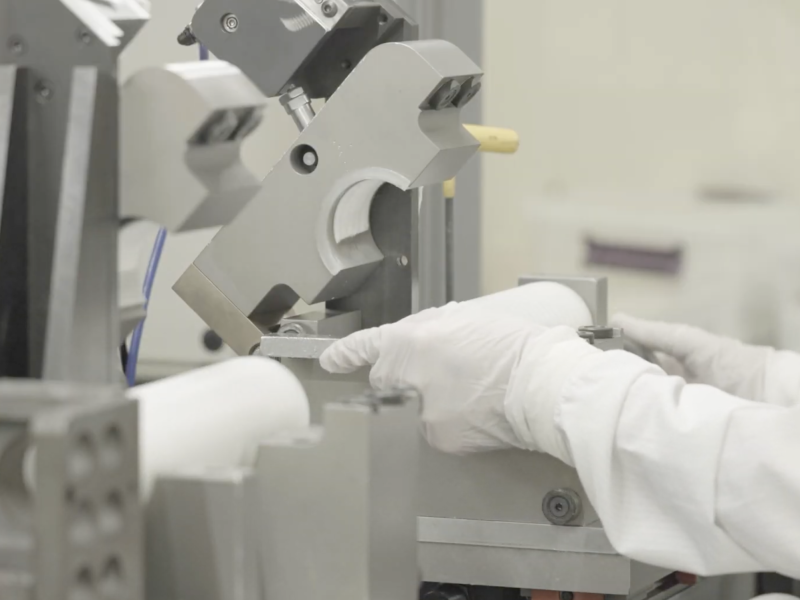
Strainrite is expanding its cleanroom by 625 square feet by the end of Q3, adding capacity for new manufacturing equipment arriving in 2027
Read More
Gamma Irradiated Clarity Capsule and Cartridge filters have successfully completed 4-year shelf-life validation testing
Read More